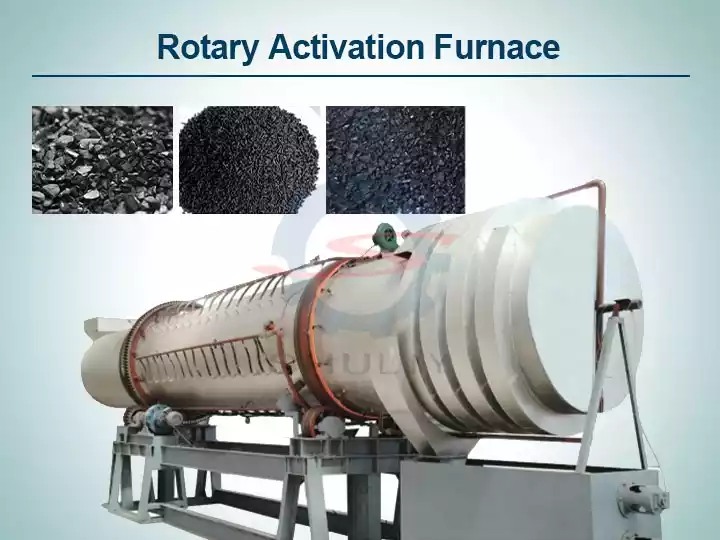
The rotary activation furnace is the core unit for physical‑method activated carbon production. Using steam as an activator at 800‑1050℃, it forms pores in the carbon feedstock and governs iodine value, methylene blue value, product yield, and production costs.
Two main types are available: the external‑heating furnace reaches 1‑2 t/d per set with flexible start‑stop, higher carbon hardness and +0.2% yield improvement. The conventional internal‑heating furnace outputs 0.15‑0.25 t/h but demands a 3‑day heat‑up period for stable operation.
Faced with concerns over startup cycle, quality, energy use, environmental performance, material and maintenance, manufacturers can find side‑by‑side comparisons, key parameters and selection advice below to match furnaces to raw‑material and capacity needs.
Core comparison of internal vs external‑heated activation furnace
| Comparison Item | External‑Heated Rotary Activation Furnace | Conventional Internal‑Heated Rotary Activation Furnace |
|---|---|---|
| Stabilization Period after Startup | Supports on‑demand start‑stop; reaches production capacity in a short time | Requires 3‑day heating‑up period to achieve stable process; frequent start‑stop is not allowed |
| Finished‑Product Yield | Lower production loss; yield is 0.2 percentage points higher | Relatively higher carbon burn‑off rate with lower yield |
| Hardness of Finished Activated Carbon | Higher particle hardness with low breakage rate | Relatively higher particle wear risk |
| Temperature Control Accuracy | Precise temperature control; compatible with flameless electric heating mode | Direct open‑flame heating causes large temperature fluctuation; heavily relies on experienced operators for commissioning |
| Equipment Footprint & Dimension | Compact overall size for easy transportation and installation | Large furnace body with heavy civil‑construction and installation workload |
| Operation Threshold | User‑friendly; operators can get competent after basic training | High operation threshold; requires on‑site support from seasoned engineers |
| Applicable Scenarios | Plants with strict environmental‑protection requirements, high‑quality carbon output needs or intermittent production mode | Large‑scale 24‑hour non‑stop continuous production pursuing high thermal efficiency |
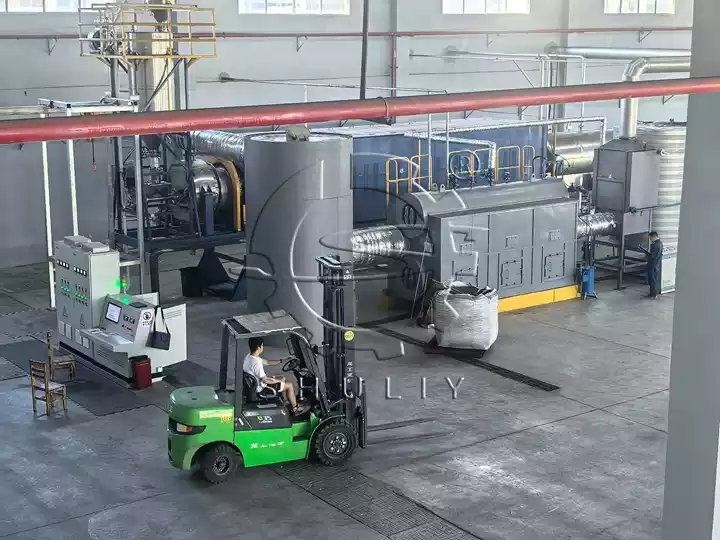
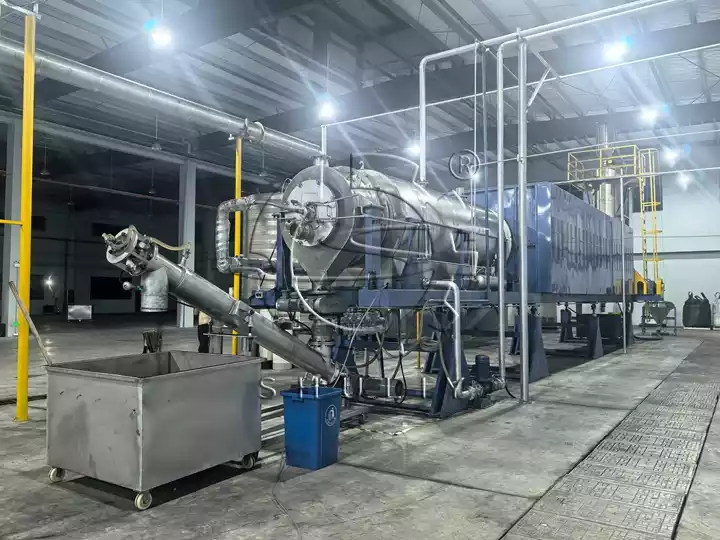
Complete production process of activated carbon activation furnace
Whole‑set physical activated carbon production workflow: Carbonized raw material → Feeding conveyor → Buffer silo → Sealed feeding device → Rotary activation furnace (steam‑based activation at 880‑1050℃) → Discharge & cooling → Elevator conveying → Crushing & desanding → Linear vibrating screen for classification and screening → Off‑spec material returns to crushing system → Qualified activated carbon goes through automatic weighing, packaging and warehousing.
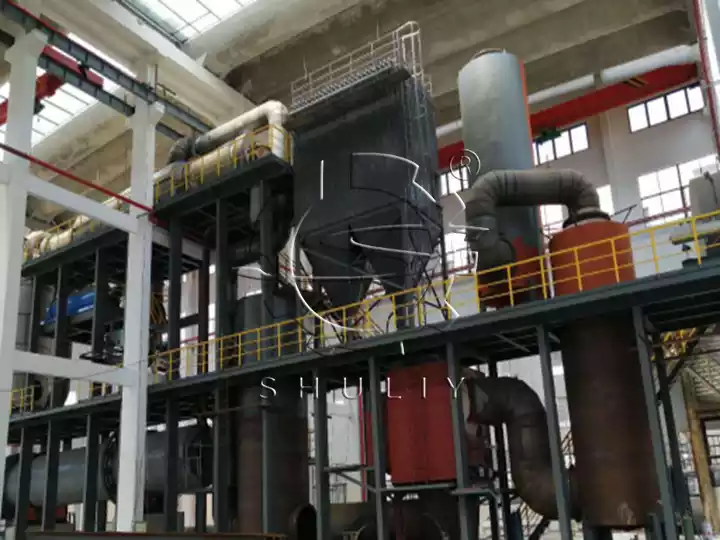
Flue‑gas environmental‑protection workflow: Exhaust gas from activation furnace → Incineration in settling combustion chamber → Flue‑gas cooling → Centrifugal dust removal → Spray tower scrubbing → Pulse dust removal → Standard‑compliant emission via chimney. The full flue‑gas treatment system meets emission standards for industrial furnace kilns.
Hard requirement for material moisture: Moisture content of incoming carbonized feedstock must be kept below 15%. Excessive moisture will trigger furnace temperature fluctuation, poor activation performance and higher steam consumption.
Working principle of the industrial rotary activation furnace
In physical‑method activated carbon production, carbonized feedstock is fed into the activation furnace. Saturated steam is injected as the activating agent. Under furnace temperatures of 880‑1050℃, gas‑solid activation reactions take place to open and expand internal pores within carbon particles, yielding porous activated carbon with a specific surface area ranging from 700‑2000 m²/g.
The activation process proceeds in three sequential phases:
- Pore‑opening Phase: Tar and amorphous carbon inside carbon particles are burnt away to unblock closed pores, with carbon burn‑off rate below 10%.
- Micropore‑forming Phase: Selective oxidation acts on carbon matrices to generate abundant micropores, ideal for manufacturing high‑iodine‑value activated carbon.
- Pore‑widening Phase: Continuous gasification‑burning of pore walls enlarges apertures and produces mesopores, suitable for activated carbon requiring high methylene‑blue value. The material burn‑off rate exceeds 50% in this phase.
Production Tip: To achieve a high iodine value (1400‑1500 mg/g), raise the activation temperature to 1050℃, reduce rotary speed, and extend material residence time, which will significantly lower product yield. For maximum yield, keep the temperature below 950℃ to produce activated carbon with iodine value <1100 mg/g.
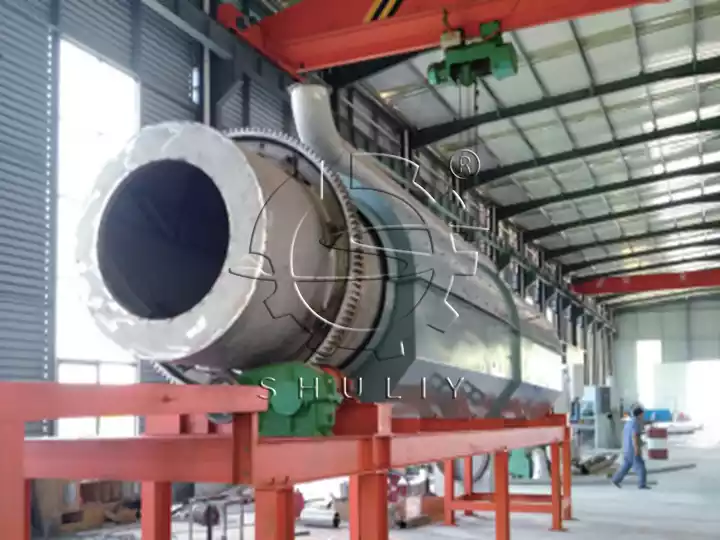
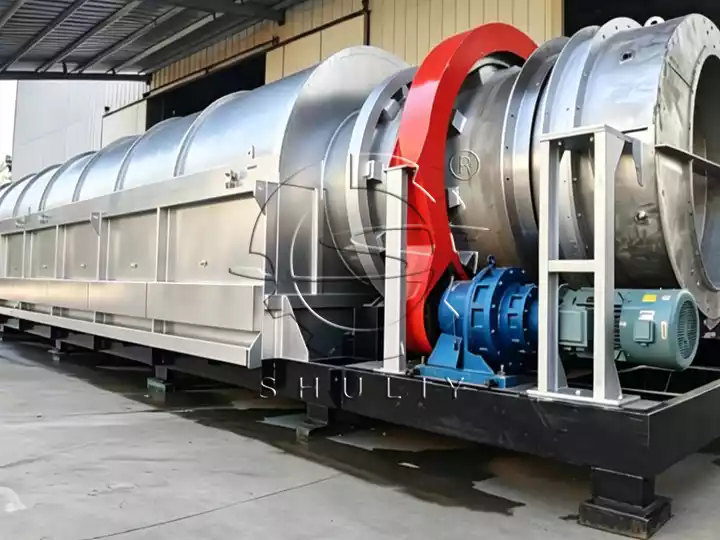
Activated carbon rotary kiln main technical parameters
Note: Parameters for furnace host only, excluding feeding, cooling, dedusting, and other auxiliary systems.
| Parameter Item | External‑Heated Rotary Activation Furnace | Traditional Internal‑Heated Rotary Activation Furnace |
|---|---|---|
| Modelo | JY‑1600 | Custom‑built rotary type |
| Cylinder Size | Φ1.6 m × L12 m | Custom dimension for different capacities |
| Cylinder Material | 310S high‑temperature resistant stainless steel;baffle plate: 8 mm 310S SS | Q235 carbon steel lined with refractory bricks |
| Activation Temperature Range | 800‑1050 ℃ | 880‑1050 ℃ |
| Material Residence Time | 60‑120 min, variable‑frequency adjustable | 60‑120 min, adjusted by rotary speed |
| Processing Capacity | 1‑2 t/d | 0.15‑0.25 t/h |
| Sealing Structure | Multi‑layer stainless steel fish‑scale seal | Ductile‑iron & refractory sealing |
| Driving System | VFD motor, big gear‑ring + supporting rollers | ZQ reducer, gear‑ring & supporting rollers |
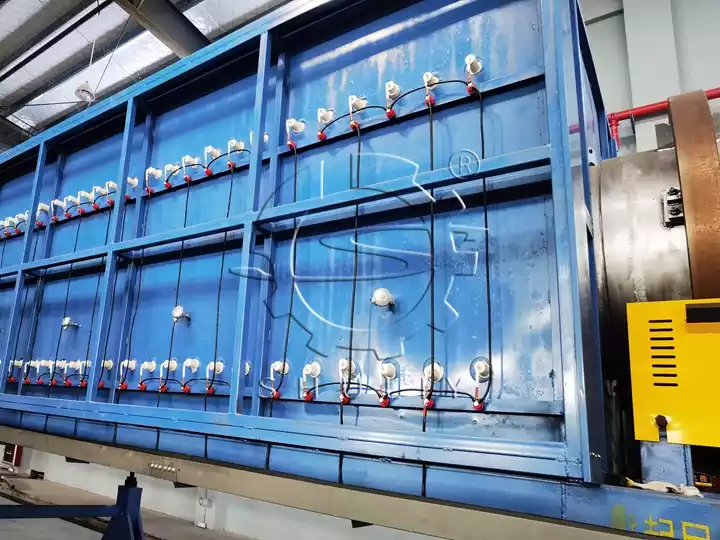
| Heating Mode | External heating (electric / gas option);no open flame inside furnace | Direct open‑flame heating inside furnace;materials contact flue gas directly |
| Temperature Control | Fast response, high adjustment accuracy | Obvious temperature lag & fluctuation |
| Operation Characteristic | Supports intermittent production, quick start‑stop | For 24‑h continuous operation;long heating‑up stabilization period, frequent start‑stop forbidden |
Advantages of the activated carbon rotary kiln
- Material durability: External‑heated rotary activation furnaces adopt 310S/316L high‑temperature‑resistant stainless steel, while internal‑heated types use carbon steel plus refractory bricks. 304 pipelines and reliable seals are preferred to extend service life and reduce material burn‑off.
- Environmental compliance: Equipped with incineration, spraying and multi‑stage dust removal systems to treat tail gas up to standard and avoid environmental rectification risks.
- Automation performance: PLC variable‑frequency control system adjusts process parameters. Optional automatic packaging cuts labor cost and human‑operation errors.
- Production supporting capacity: Enclosed conveying equipment reduces workshop dust. A sand remover lowers ash content and improves finished activated carbon quality.
- Technical service & investment: Select manufacturers offering free operator training. Budget shall cover extra costs including freight, installation and taxes.
Rotary activation furnace operation and maintenance
- Pre‑start: Ensure equipment and water pressure ≥1.5 kg are normal. Feedstock moisture<15% before heating.
- Heating & Feeding: Drain condensate before steam‑in at 750℃; feed after 20‑min constant 800℃. Operating temp:880‑950℃, steam pressure:3.5‑4kg.
- Temp‑drop Troubleshooting: Check water supply & fans for sharp drop; check feed shortage & steam pressure for slow drop. Wait 20 min after valve adjustment, avoid frequent big tuning.
- Slag Removal: Clean furnace‑wall slag every 7‑10 days with high‑temp PPE. Heavy slag damages furnace and cuts output.
- Wearing Parts: Inspect fish‑scale seals & steam pipes. Replace leaking parts timely to prevent carbon over‑burning.
How to select an activated carbon activation furnace?
- Production Capacity Requirement: Choose external‑heated rotary activation furnace for 1‑2 tons of daily output. For 24‑hour continuous large‑capacity production, internal‑heated furnace is available. Multiple furnaces in parallel can boost total output.
- Product Positioning: External‑heated furnace is preferred for high‑grade nut‑shell activated carbon, strict environmental‑protection requirements and intermittent production. Internal‑heated furnace fits mass‑grade carbon with year‑round continuous operation.
- Raw Material Condition: Moisture content of char feedstock shall be ≤15%. Desanding equipment is required for high‑ash raw materials to reduce ash content of final products.
- Overall Investment Evaluation: Do not compare price only on main furnace. Total investment covers main unit, auxiliary equipment, transportation, installation, civil construction, steam & water circulation system. Verify supplier’s technical training and after‑sales support.
There is no single best choice between internally heated and externally heated rotary activation furnaces. Your capacity, product positioning, and production mode matter most. Check the cylinder material, sealing structure, and support configuration before you buy. For more carbon processing equipment, please visit our carbonization furnace equipment page.